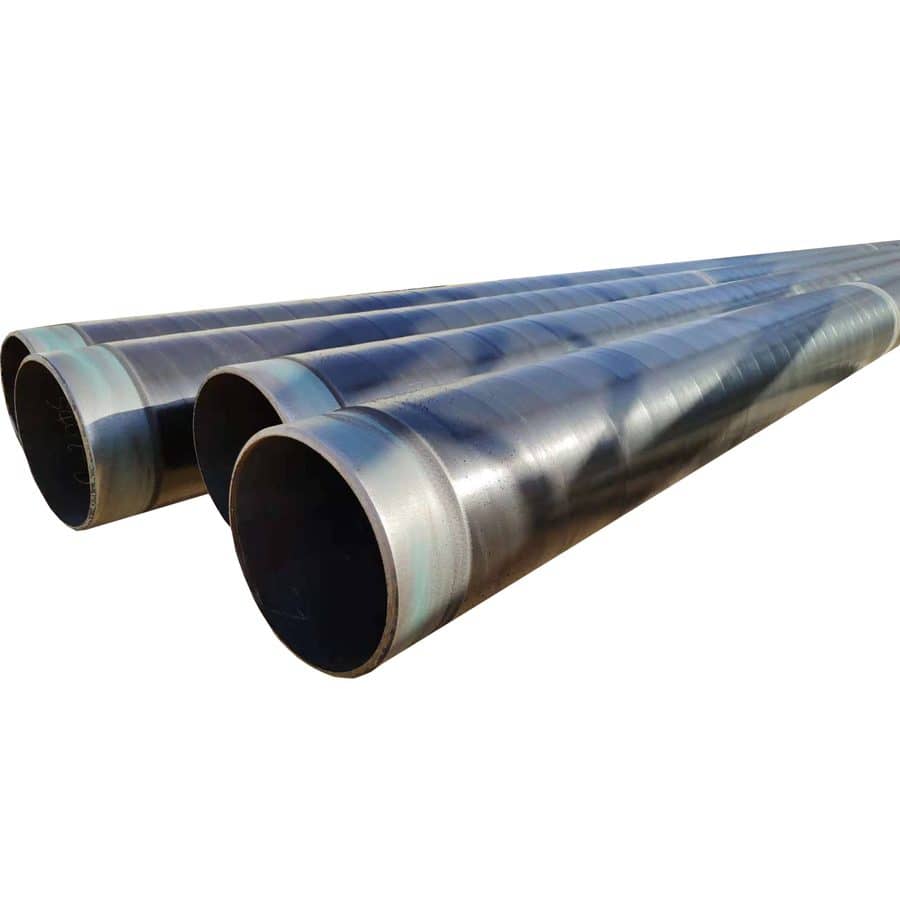
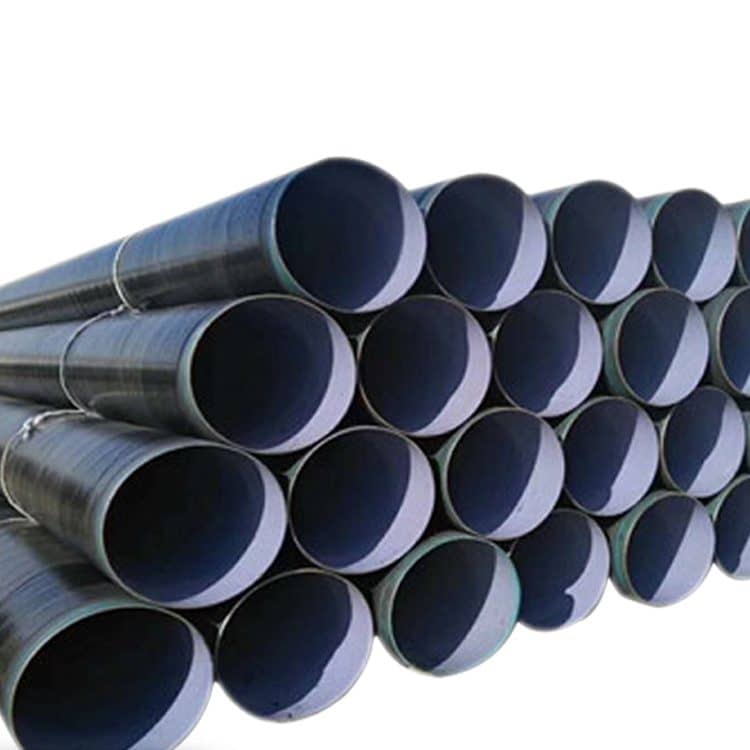
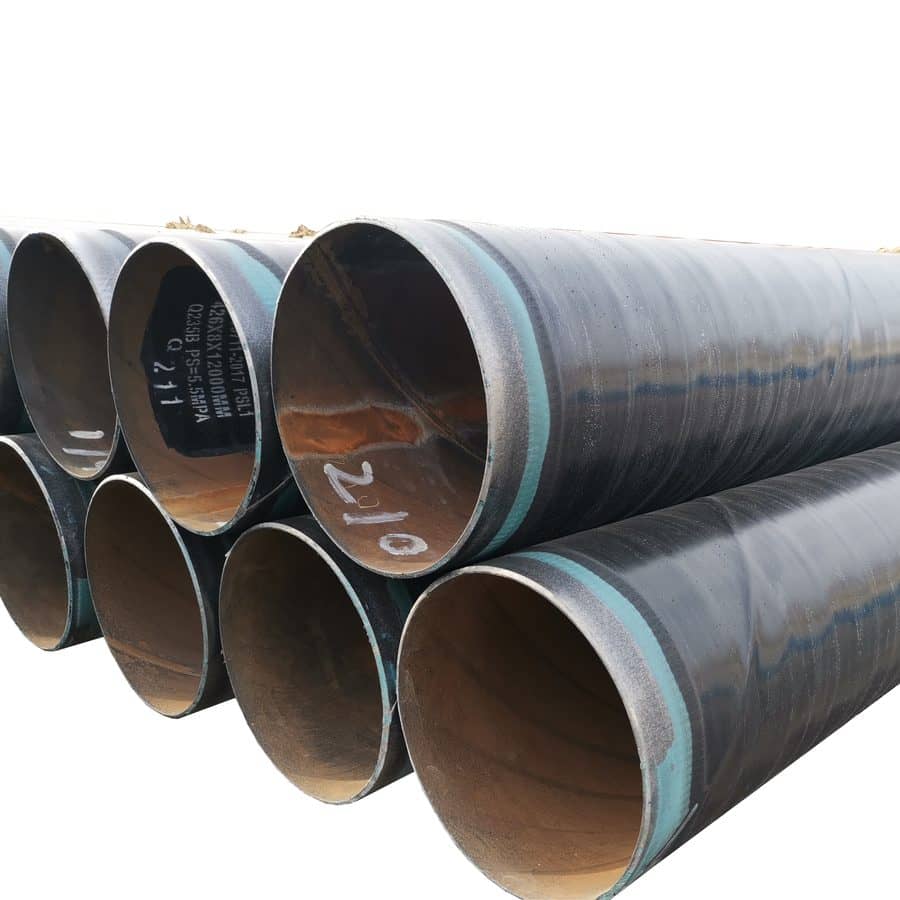
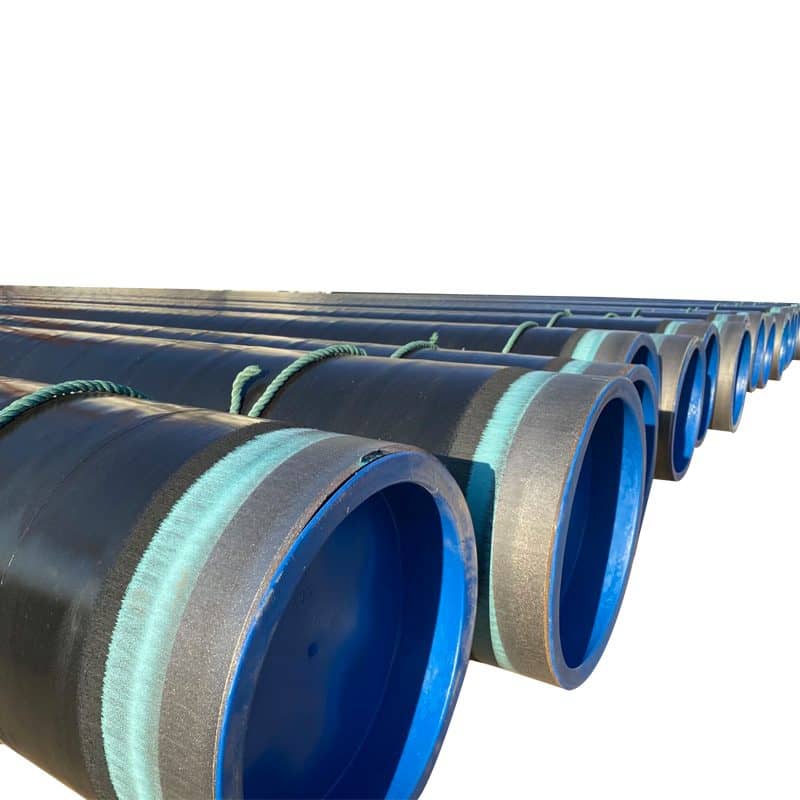
3-layer PE / TPEP external anti-corrosion for buried pipelines, applied on our own coating line.
3PE anti-corrosion pipe is the standard protection for buried steel pipelines carrying water, oil or gas. The system is built in three layers: a fusion-bonded epoxy (FBE) primer that bonds to the blast-cleaned steel, a copolymer adhesive, and an extruded polyethylene top coat that carries the mechanical and chemical load.
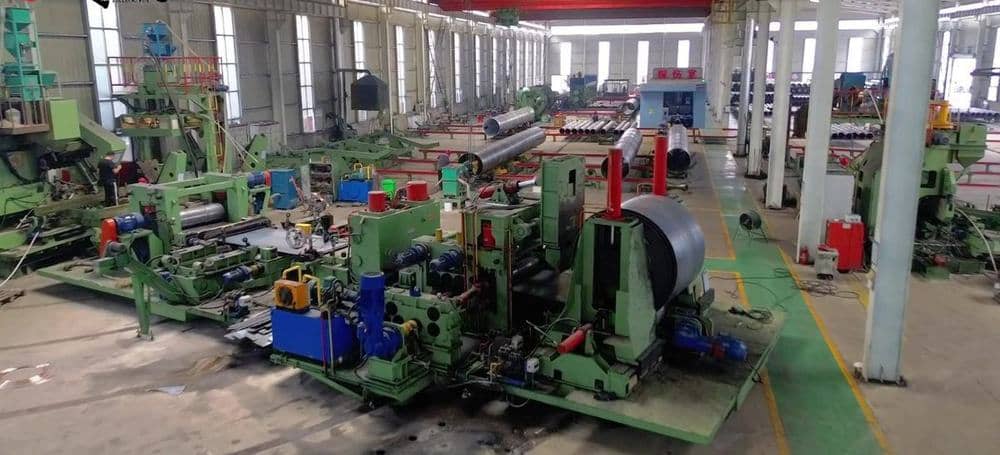
The quality of a 3PE coating is decided before the coating is applied. We shot-blast the pipe to Sa 2.5, control the anchor profile, heat the pipe to the specified temperature by induction, then apply FBE by electrostatic spray, adhesive and PE by side or cross-head extrusion, followed by water cooling and end trimming.
Inspection is done on the line and in the lab: holiday detection over the whole coated surface, thickness measurement, peel strength at the specified temperature, cathodic disbondment, impact resistance and indentation. Batch records are archived with the heat numbers.
We also supply TPEP — epoxy coating inside and outside — where the internal lining must protect water quality or reduce flow resistance. Internal epoxy can be supplied to drinking-water contact requirements.
| Base Pipe | SSAW / ERW / seamless per order |
| Outside Diameter | 219 – 3820 mm (DN200 – DN3800) |
| Coating Structure | 3PE / 2PE / FBE / TPEP |
| Total Coating Thickness | 2.0 – 3.7 mm (ordinary to heavy grade) |
| Surface Preparation | Shot blasting to Sa 2.5, anchor profile 50–90 μm |
| Operating Temperature | -40 °C to +80 °C (PE top coat) |
| Holiday Detection | 100% of coated surface, per standard voltage |
| Standard | GB/T 23257, SY/T 0413, DIN 30670, CSA Z245.21 |
| Coating Capacity | Approx. 200,000 m² / year |
| Certificate | MTC EN 10204 3.1 + coating inspection report |
Every pipe passes through the same controlled route, with inspection points at each stage.
Check dimensions and surface, remove oil and moisture, pre-heat before blasting.
Abrasive blasting to near-white metal with controlled anchor profile for coating adhesion.
The pipe is heated uniformly to the FBE application temperature window.
Fusion-bonded epoxy powder is applied evenly as the corrosion-resistant primer.
Copolymer adhesive and PE top coat are extruded over the epoxy layer and rolled.
Water quench, then coating ends are trimmed to the specified weld-stub length.
100% holiday detection plus batch tests for thickness, peel strength and cathodic disbondment.
Double-sided submerged arc spiral welded pipe for water, structure and piling.
Direct-buried polyurethane pre-insulated pipe for district heating networks.
Steel-jacket steam insulation for high-temperature steam transmission.
Plastic-coated pipes for water supply, fire fighting, mining and cable protection.